High-Voltage Interconnects for Aerospace
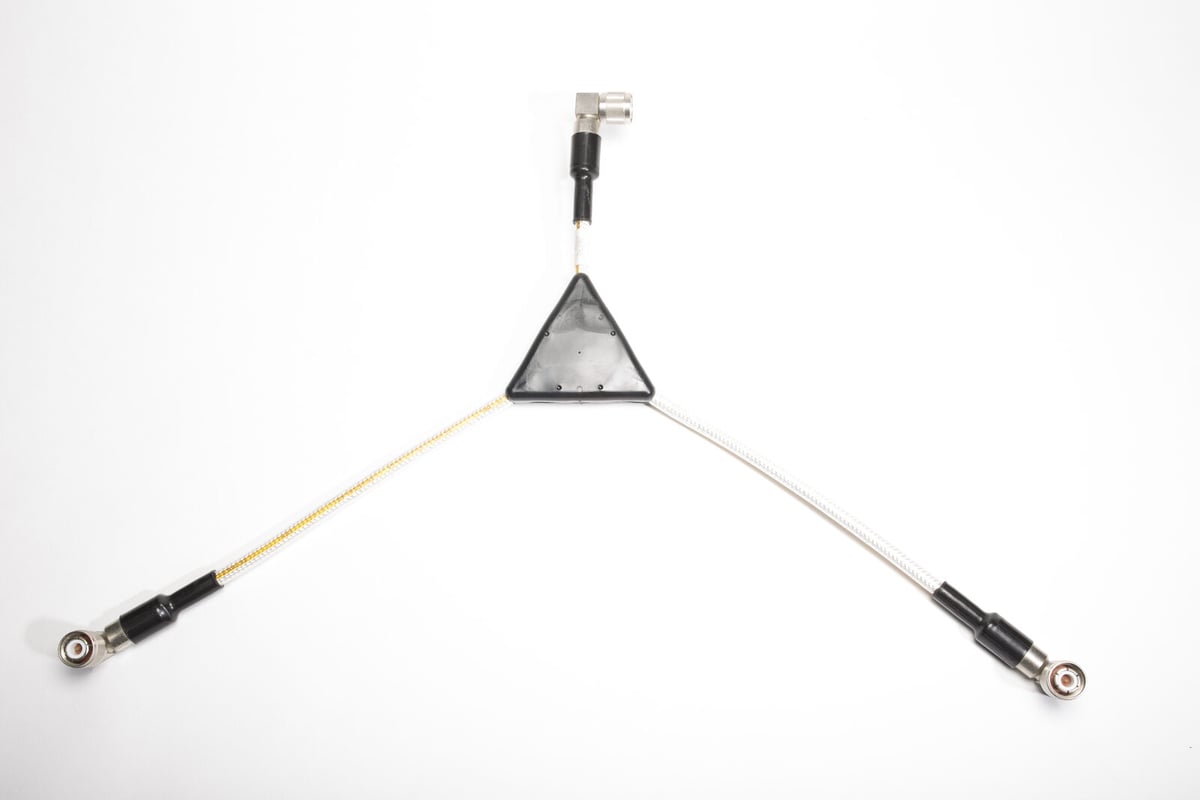
Caton designs and manufactures custom high-voltage cable assemblies and RF interconnect for commercial and military aerospace platforms — avionics, satellite communications, airborne command and control, aerostat surveillance, and aircraft electrical systems. AS9100 certified, ITAR registered, with the engineering continuity that long-program-life aerospace platforms require. Engineering-led since 1973.
The engineering team responsible for the high-voltage interconnect, across the program lifecycle
We are the engineering team responsible for the high-voltage interconnect on aerospace platforms where the part qualified at design release has to be available, identical, and engineering-supported decades later. Our customers come to us when off-the-shelf connectors won’t hold the qualification, when the program needs an engineering-accountable supplier with full design ownership, or when a fielded platform needs sustainment from a US-based, AS9100-certified manufacturer.
We own the full interconnect: cable design, connector design, in-house overmolding, and complete electrical qualification under one roof — across the program lifecycle, from design release through sustainment and obsolescence management.
High-voltage and RF design, qualification, and configuration control
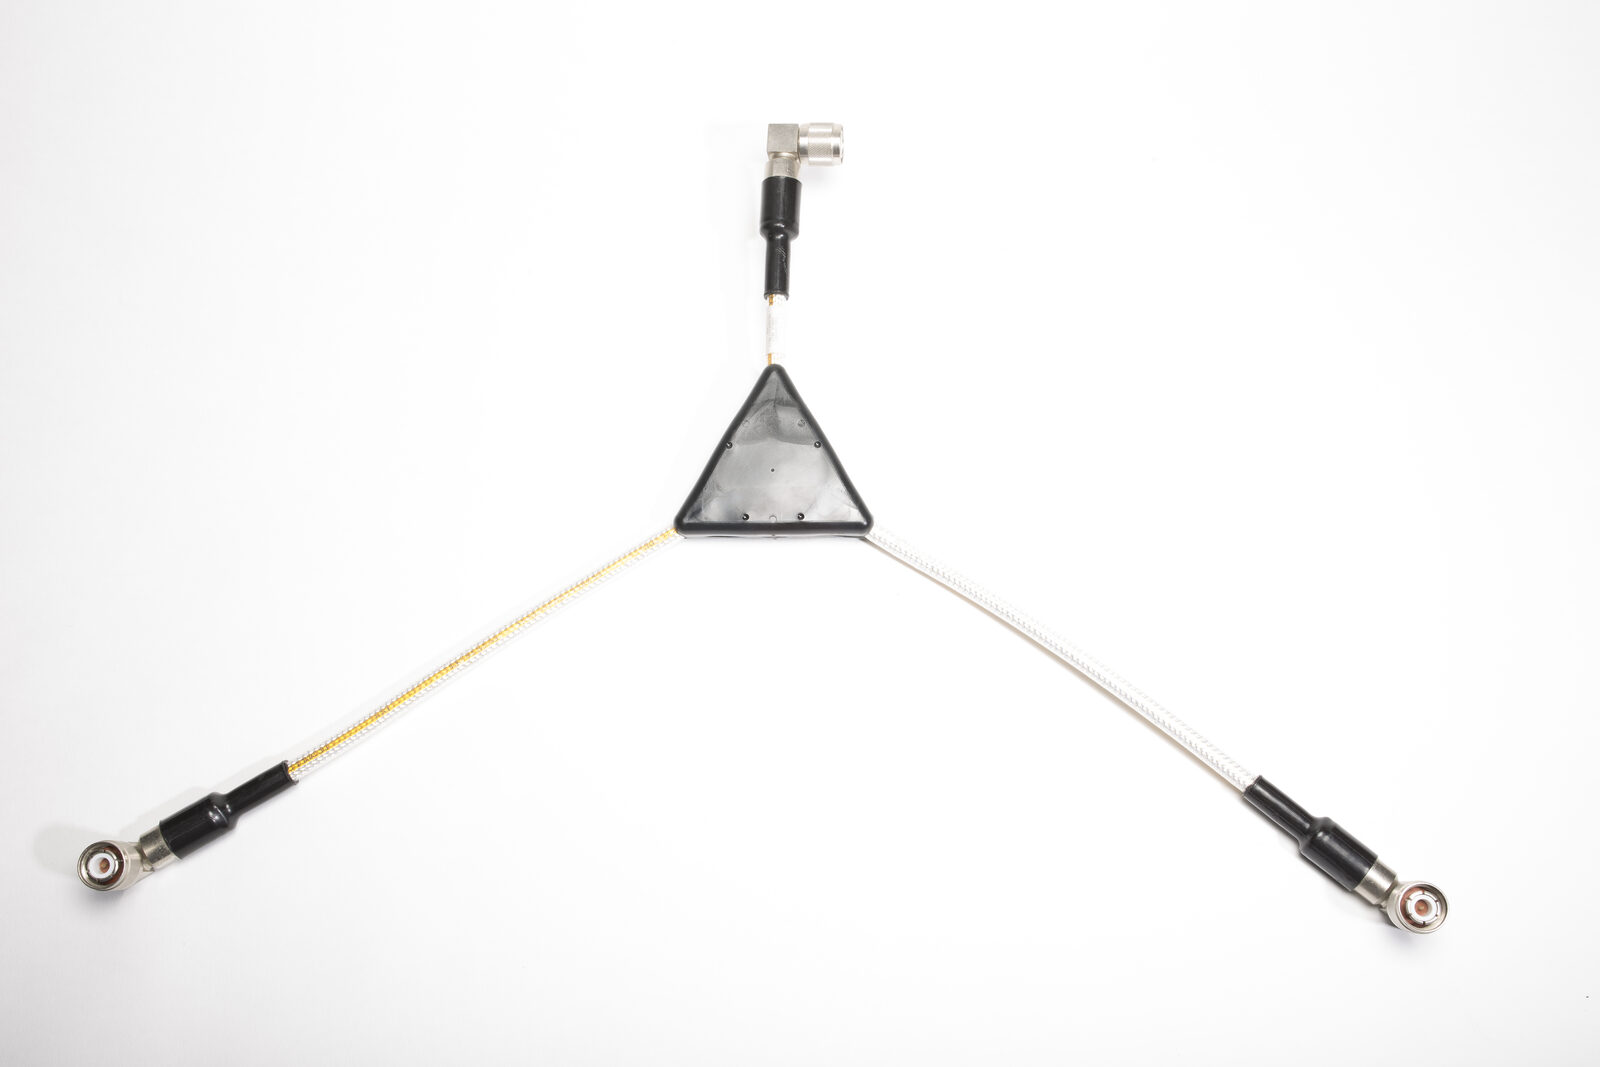
Custom interconnect engineered to the aerospace qualification regime — not adapted from commercial parts. RF distribution, high-voltage signal and power, multi-port custom geometries, and integrated mechanical features for airframe mounting, all designed under AS9100 controlled processes.
Custom cable and connector design from 1 kV to 250 kV, plus RF distribution and signal interconnect. Finite element analysis using Electro V10.2 for electrical field optimization, corona mitigation, and dielectric stress analysis at altitude.
Overmolded interconnects engineered for the airframe environment — vibration, thermal cycling, altitude derating, and long-term insulation aging. Overmold geometry, materials, and processing are part of the electrical design.
Corona inception and extinction, partial discharge, hi-pot, insulation resistance, dielectric withstand, leakage current, and thermal cycling — all in-house. Altitude testing to 70,000 ft in our Tenney altitude chamber, including corona-at-altitude characterization. Manufacturing engineers work at benches on the production floor, alongside the test stations and the build, so design issues get caught and resolved in real time.
Caton designs to and manages qualification programs against the standards aerospace programs require — DO-160 airborne environmental, MIL-STD-461 EMI/EMC, MIL-STD-810 environmental, MIL-STD-704 aircraft electrical power, NASA EEE-INST-002 for space, and AS9102 first article inspection. Environmental qualification is conducted at accredited test labs as part of the program engagement, with Caton managing the test plan, witnessing, and report integration.
Locked configurations at design release. Controlled change management. Build records, material certifications, and test data archived for the life of the program. Risk-based thinking under AS9100. Counterfeit electronic parts mitigation under AS5553.
PEEK, FEP, silicone, stainless steel, and aerospace-grade alloys selected per application and qualified per program. Materials decisions made by Caton engineering, not driven by catalog availability.
Where Caton interconnect is specified today
Aerospace relationships sustained across decades of program lifecycles


Components specified into commercial aerospace avionics, satellite communications platforms, airborne command and control systems, and aerostat surveillance programs. Specific program references available under appropriate disclosure.
Engineering continuity for programs that run for decades
Aerospace programs run for decades. The cable assembly qualified at design release has to be available, identical, and engineering-supported in year twenty. Locked configurations, controlled change management, and same-team engineering across the program lifecycle.
Every Caton assembly ships with material certifications, process records, electrical test data, and configuration control records. AS9102 first article inspection on new programs. Build records archived for the life of the program.
When a component goes end-of-life or a process changes, Caton’s engineering team manages the transition under controlled change. Customers don’t lose the qualification because a sub-tier vendor discontinued a part.
Family-owned, US-manufactured, AS9100-certified, ITAR-registered. The same engineering team across decades of aerospace programs. The supplier you qualify today is the supplier still building your part in year twenty.
Working with Caton on an aerospace program
We’re built for the design phase of new aerospace programs and for the sustainment phase of fielded platforms where the original supplier can no longer build, qualify, or support the part. We respond to RFQs at the development, qualification, and production stages, and we support sustainment, obsolescence management, and configuration recovery on legacy programs.
Explore other industries we serve
Talk to engineering about your aerospace program
Your design engineer talks to our design engineer. New program development, qualification, sustainment, or obsolescence management on fielded platforms — the conversation starts at the engineering bench.