High-Voltage Interconnects for Defense
Caton designs and manufactures custom high-voltage cable assemblies and connectors from 1 kV to 250 kV for missile defense, directed energy, pulsed power, hypersonic propulsion, airborne command and control, and space-based defense systems. Engineering-led since 1973.
The engineering team responsible for the high-voltage interconnect
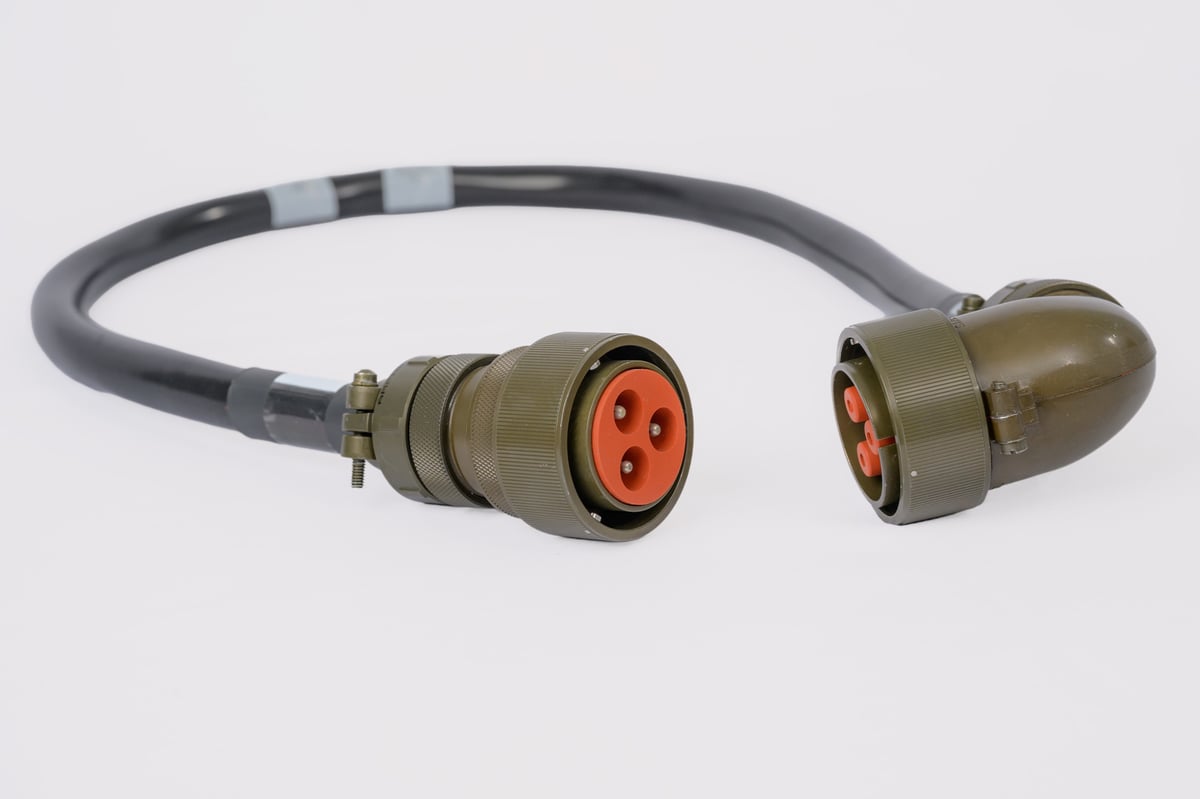
We are the engineering team responsible for the high-voltage interconnect on systems where the cable assembly is part of the weapon, not an accessory to it. Our customers come to us when corona inception, partial discharge, dielectric stability under thermal cycling, altitude derating, or long-term insulation aging will determine whether the system performs to specification — and when an off-the-shelf connector won't get them there.
We own the full interconnect: cable design, connector design, in-house overmolding, and complete electrical and environmental qualification under one roof. We do not subcontract the parts of the assembly that determine whether it works.
High-voltage design, qualification, and manufacturing under one roof
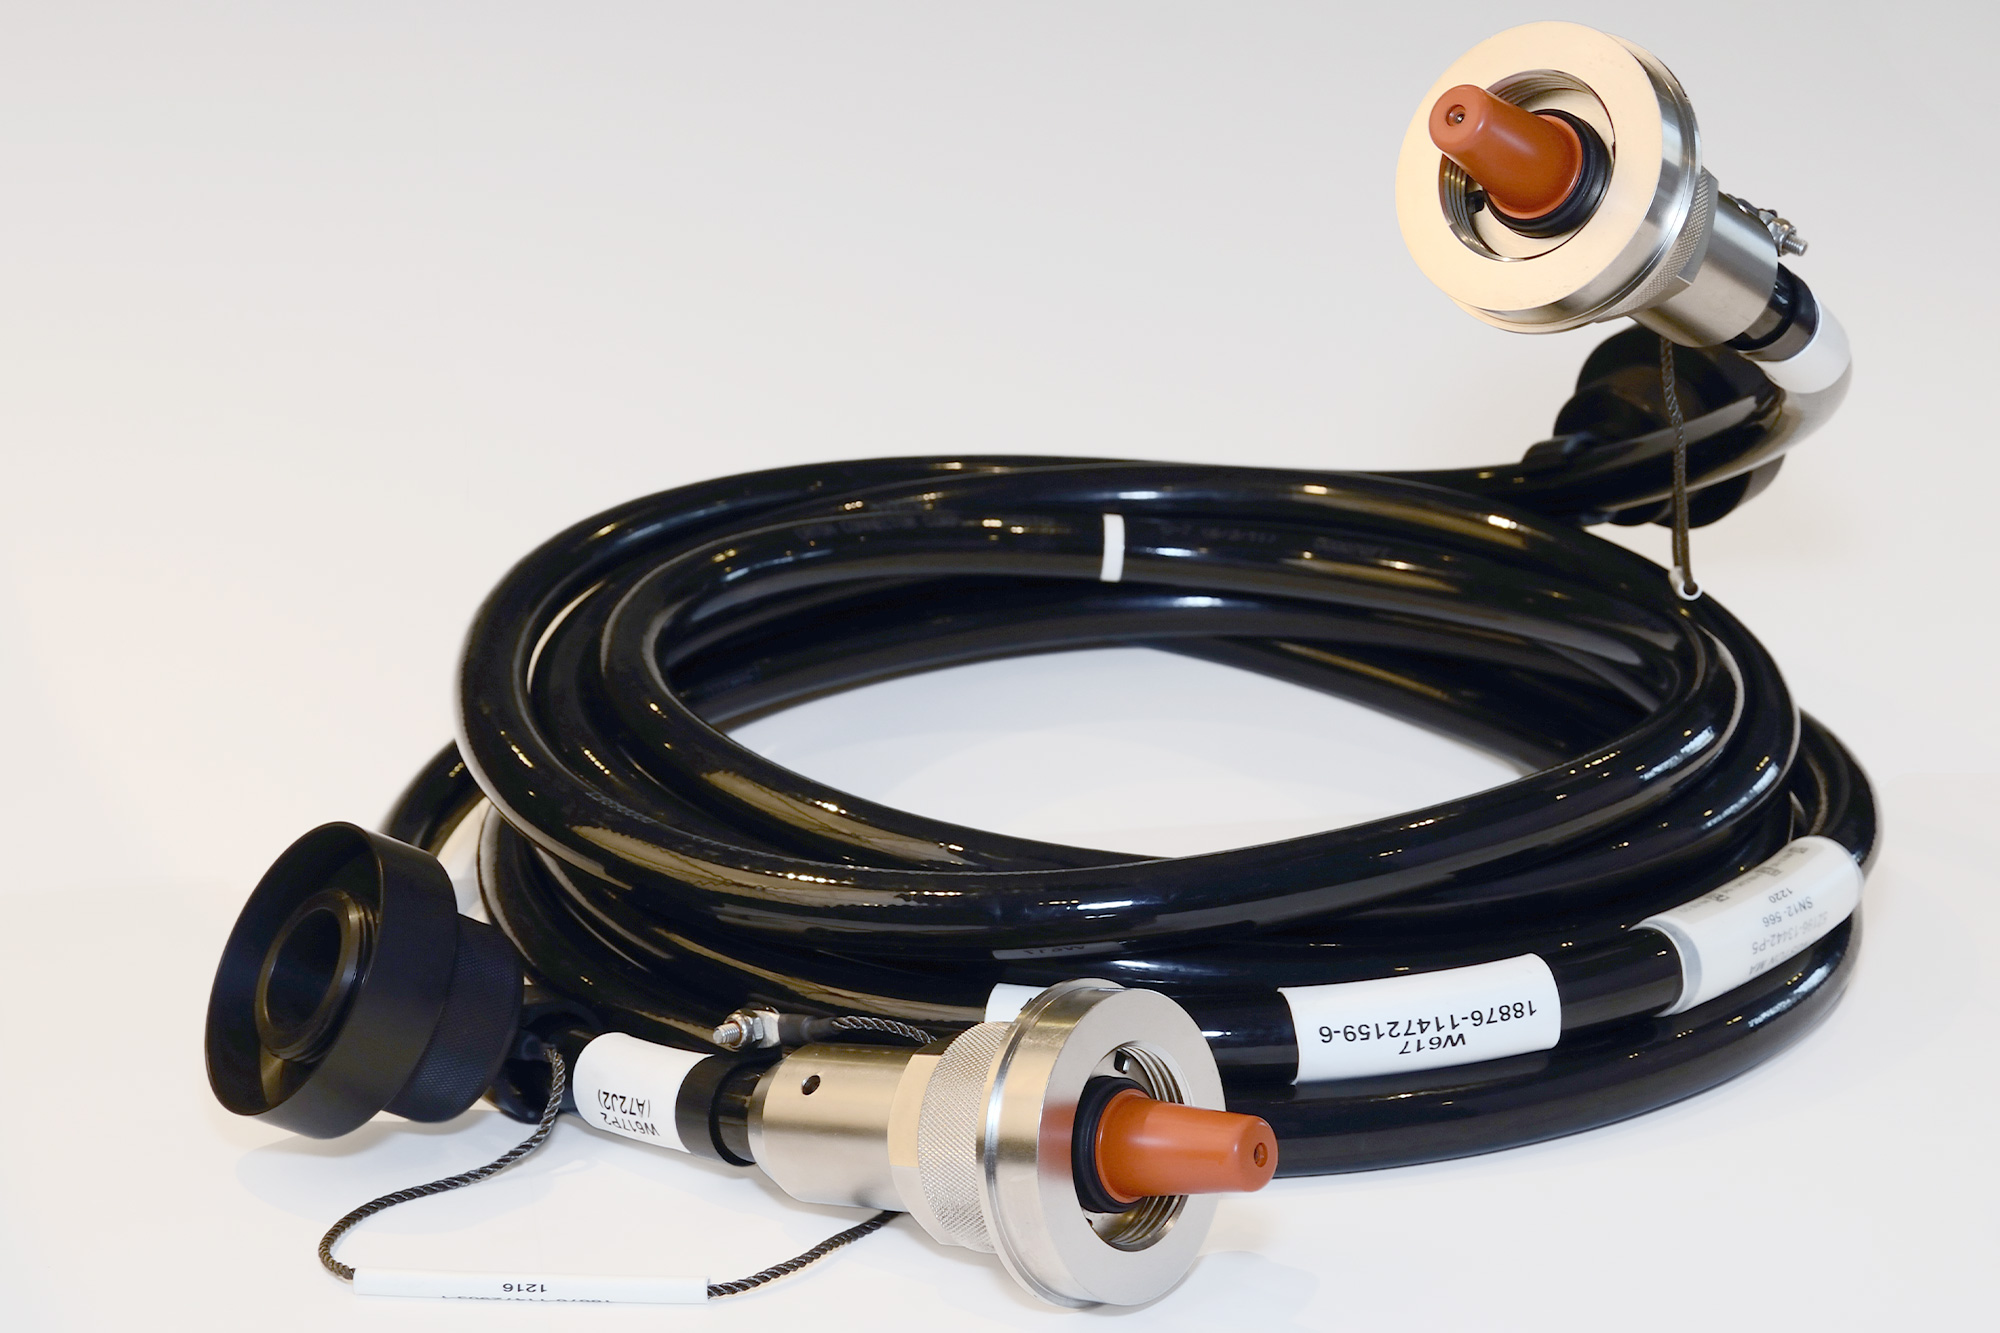
Custom geometry — right-angle backshells, in-line transitions, sealed feedthroughs — engineered to fit the airframe, the vacuum chamber, or the missile body. We design the interconnect for the system, not the system around the interconnect.
Custom cable and connector design for applications from 1 kV to 250 kV. Finite element analysis using Electro V10.2 for electrical field optimization, corona mitigation, and dielectric stress analysis. Materials selection driven by application, not catalog availability.
Overmolded interconnects engineered for the application — not adapted from commercial parts. Overmold geometry, materials, and processing are part of the electrical design, not a finishing step.
Corona inception and extinction, partial discharge, hi-pot, insulation resistance, dielectric withstand, leakage current, and thermal cycling — all in-house. Altitude testing to 70,000 ft in our Tenney altitude chamber, including corona-at-altitude characterization. Manufacturing engineers work at benches on the production floor, alongside the test stations and the build, so design issues get caught and resolved in real time.
Caton designs to and manages qualification programs against the standards defense programs require — MIL-STD-461 EMI/EMC, MIL-STD-810 environmental, MIL-STD-1576 ordnance, NASA EEE-INST-002 for space, and AS9102 first article inspection. Environmental qualification is conducted at accredited test labs as part of the program engagement, with Caton managing the test plan, witnessing, and report integration. Risk-based thinking under AS9100. Counterfeit electronic parts mitigation under AS5553.
Where Caton interconnect is specified today
Specified into mission-critical defense and aerospace programs


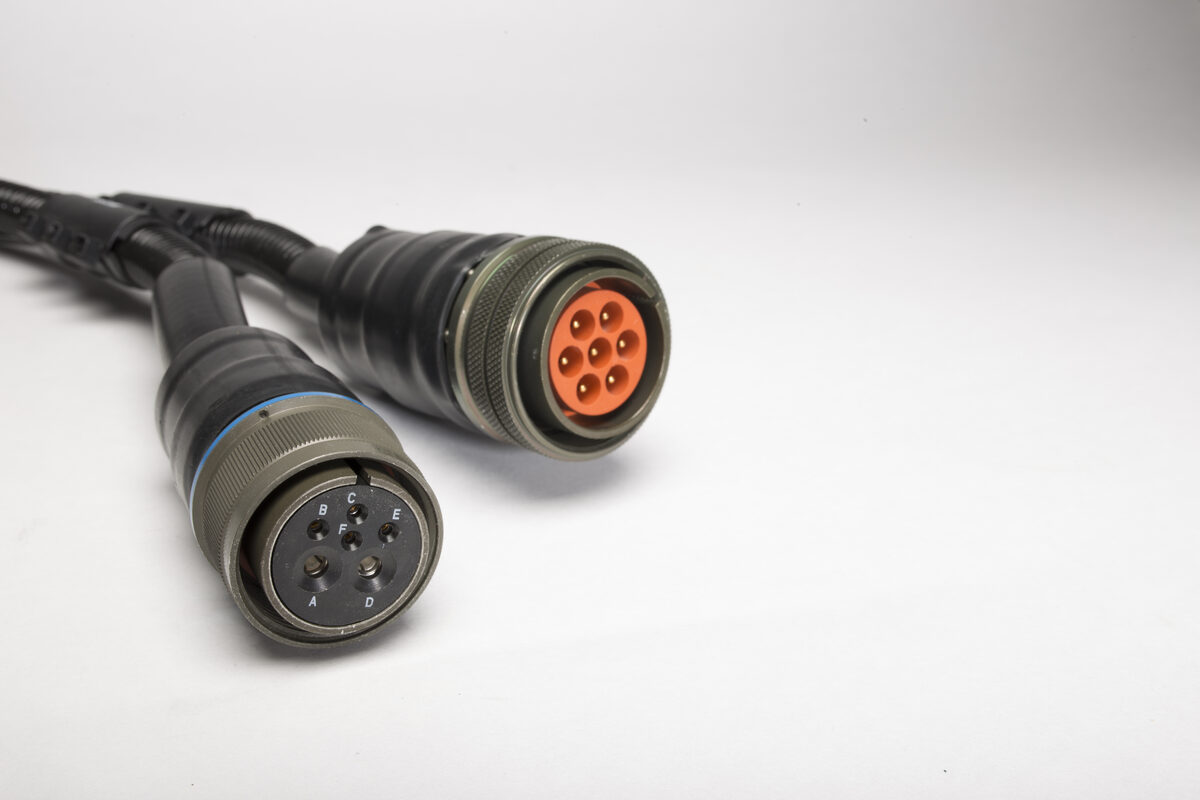
Components specified into airborne command and control platforms, missile defense radar systems, and commercial and military aerospace programs. Specific program references available under appropriate disclosure.
Engineering accountability, not vendor management
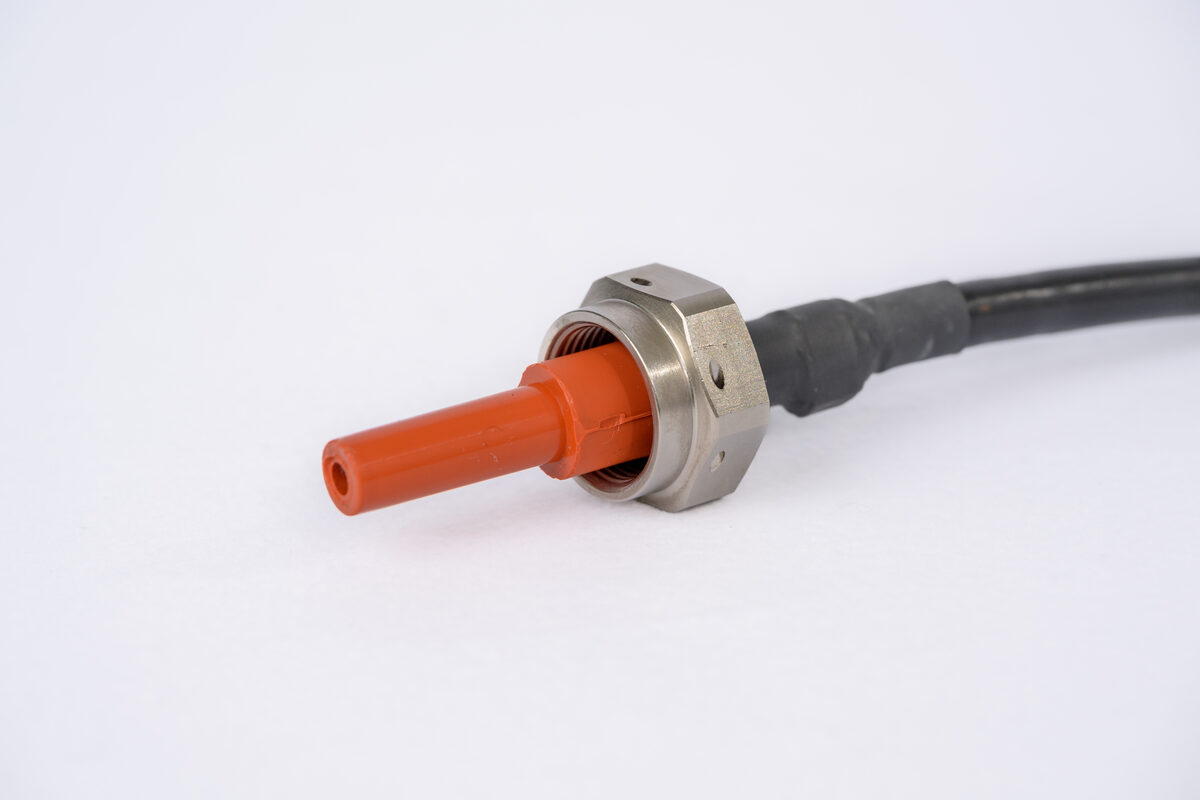
When the connector and the cable are designed by different vendors, the failure mode lives at the interface and nobody owns it. Caton designs and qualifies both, so the high-voltage performance of the assembly is one engineering team's responsibility — not a handoff.
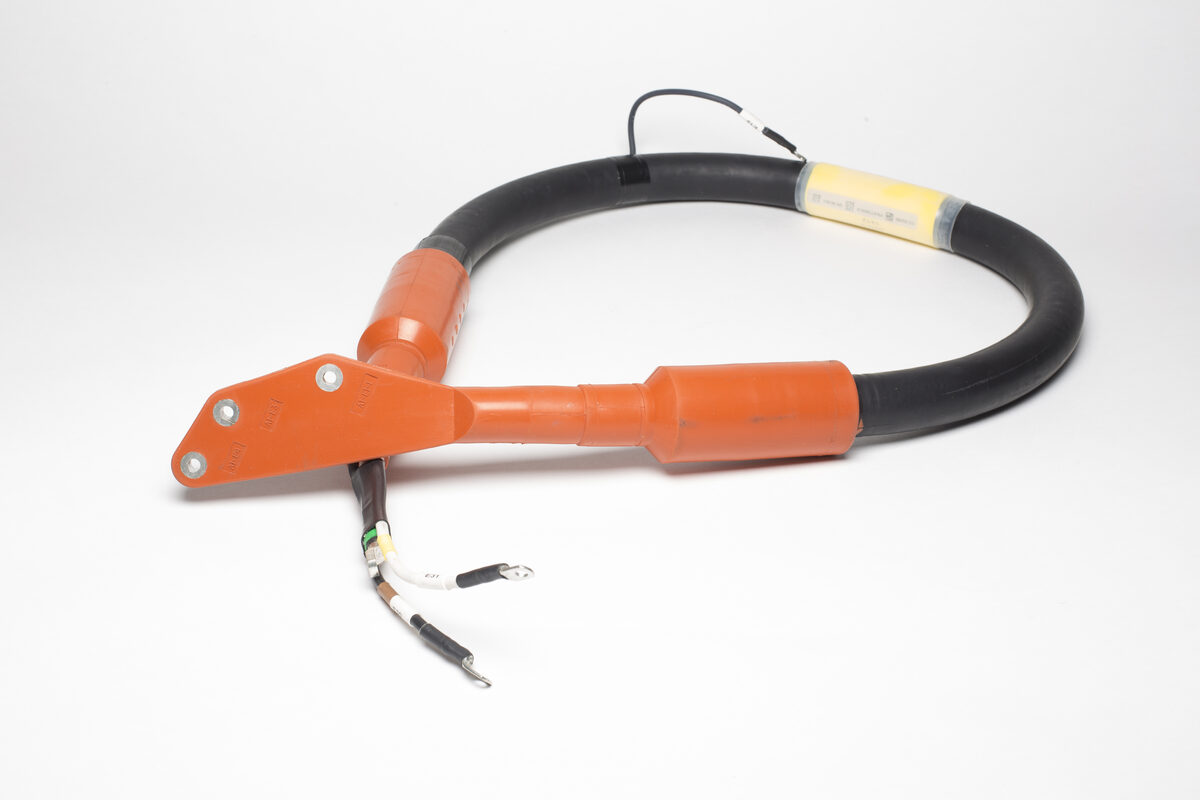
Custom HV cable assembly with overmolded splice geometry and integrated mounting hardware. The same engineering team designs the cable, the overmold, and the termination — one continuous dielectric path, one accountable supplier.
When the connector and the cable are designed by different vendors, the failure mode lives at the interface and nobody owns it. We design both, qualify both, and stand behind both.
Corona, partial discharge, hi-pot, altitude to 70,000 ft in our Tenney chamber, and thermal cycling — all in-house. Manufacturing engineers on the production floor catch design issues at the bench, in real time.
Your design engineer talks to our design engineer. The answer comes from the person who can change the design, not from an account manager who has to check with engineering and call you back.
Defense programs run for decades. The cable assembly qualified at EMD has to be available, identical, and engineering-supported in year fifteen. Locked configurations, controlled change management, and same-team engineering since 1973.
Working with Caton on a defense program
We're built for the design phase of new programs and for the recovery phase of programs where the incumbent supplier can't hold qualification. The earlier we're engaged, the more design margin we can build in. We routinely respond to RFQs for development programs at the breadboard, brassboard, and EMD stages, and we support production, sustainment, and obsolescence management.
Explore other industries we serve
Talk to engineering about your defense program
Your design engineer talks to our design engineer. New program development, qualification recovery, sustainment, or obsolescence management — the conversation starts at the engineering bench.