High-Voltage Interconnects for Industrial Applications
Caton designs and manufactures custom high-voltage cable assemblies and test leads from 5 kV to 50 kV operating, qualified to 100 kV hi-pot, for HV test equipment OEMs and HV power supply manufacturers — where corona-free performance, semiconductive-layer construction, and operator-handled durability determine whether the equipment ships on schedule and survives in the field. Engineering-led since 1973.
The engineering team responsible for the high-voltage interconnect
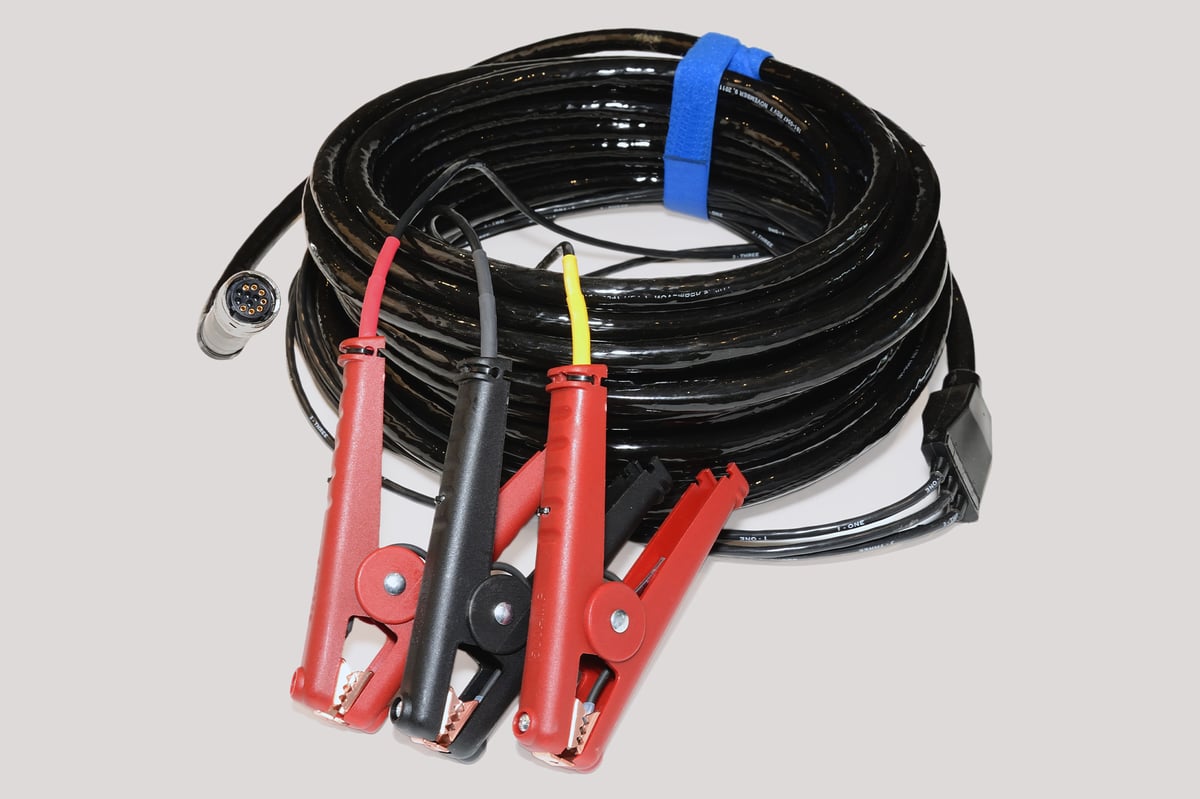
We are the engineering team responsible for the high-voltage interconnect on industrial test equipment and HV power supplies where corona inception, dielectric stress grading, and operator-handled durability determine whether the equipment qualifies, ships, and holds up in the field. Our customers come to us when an off-the-shelf cable won't hold at the operating voltage, when long test-lead runs require semiconductive-layer construction the catalog houses don't offer, or when the program's incumbent supplier can't deliver overmolded terminations that survive substation handling.
We own the full interconnect: cable design, connector design, in-house overmolding, semiconductive-layer integration, and complete electrical qualification under one roof. We do not subcontract the parts of the assembly that determine whether it works.
Corona-free design, semiconductive-layer integration, and field-shaped overmolding
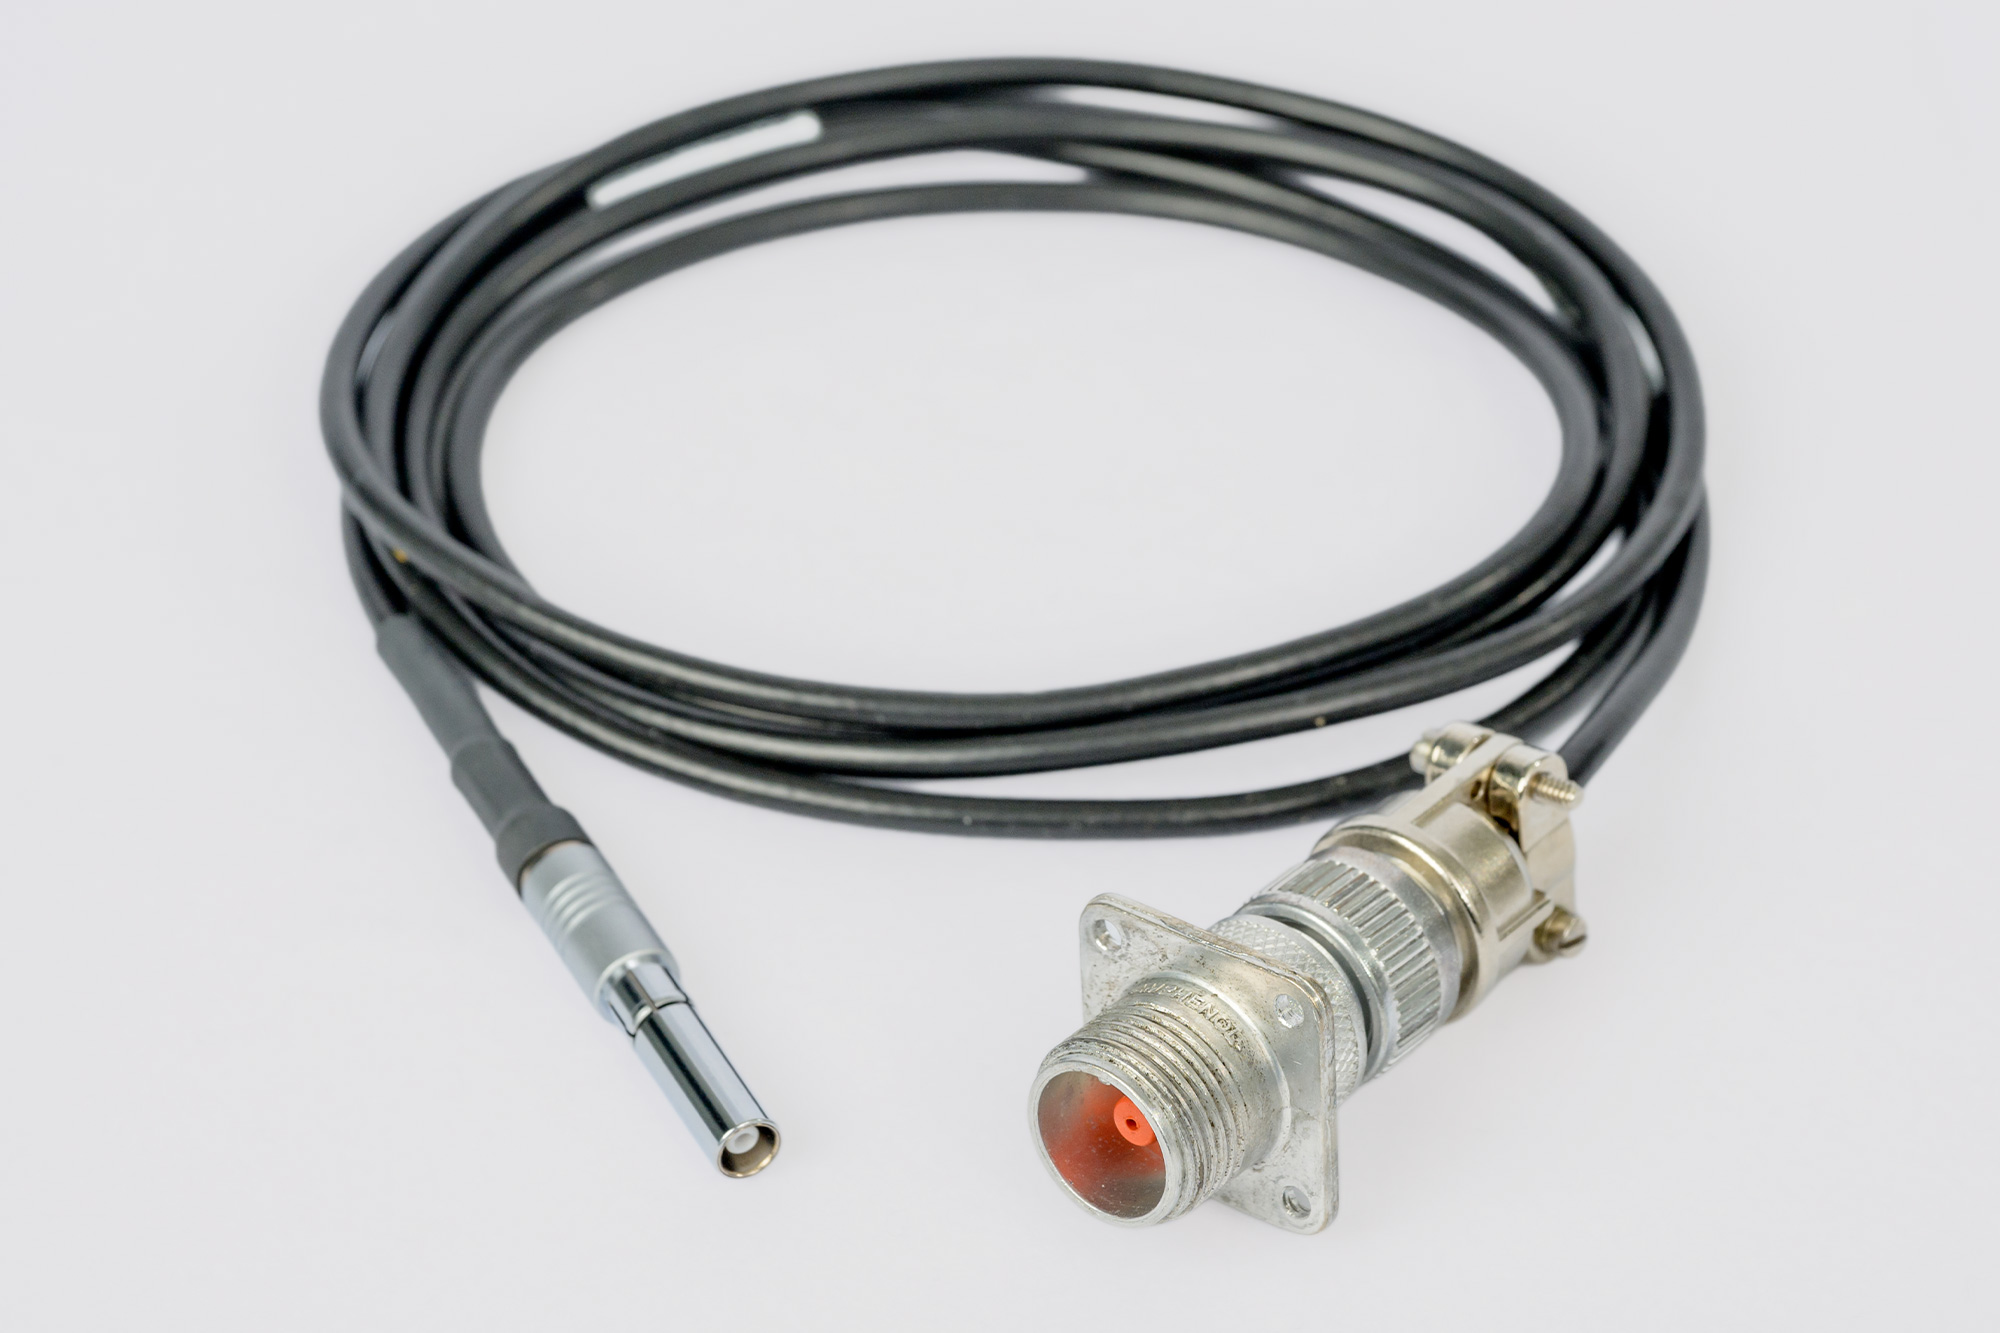
HV cable engineered with a semiconductive layer over the insulation to grade dielectric stress along the length and at terminations — the construction that makes long test-lead runs viable at 50 kV without corona on the conductor or at the boot. Custom geometries and overmold profiles engineered for the application, not adapted from commercial parts.
Custom cable and connector design from 5 kV to 50 kV with corona inception margin engineered into the geometry, not assumed. Finite element analysis using Electro V10.2 for electric field optimization and partial discharge mitigation. Materials selection driven by the dielectric environment — air, oil, or potted — not catalog availability.
Field-shaped overmolded terminations engineered for the application, not adapted from commercial parts. Overmold geometry, durometer, and material are part of the electrical design — they determine where corona inception happens at the cable-to-connector interface and how the boot survives operator handling in the field.
HV cable construction with a semiconductive layer over the primary insulation to grade dielectric stress and suppress corona along long cable runs and at terminations. The construction enables 50 kV operation in flexible test leads where bare-insulation designs corona on the conductor surface or at the boot interface.
Corona inception and extinction, partial discharge, hi-pot to 100 kV, insulation resistance, dielectric withstand, leakage current, and thermal cycling — all in-house. Manufacturing engineers work at benches on the production floor, alongside the test stations and the build, so design issues get caught and resolved in real time.
Representative electrical and environmental capability
| Specification | Value |
|---|---|
| Operating voltage range | 5 kV to 50 kV DC (standard); to 100 kV (custom) |
| Hi-pot test voltage | Up to 100 kV DC |
| Partial discharge | < 5 pC at 50 kV DC |
| Cable construction | Semiconductive layer over insulation for stress grading |
| Operating temperature | −40°C to +90°C |
| Flammability rating | UL 94 V-0 (cable jacket and overmold materials) |
| Insulation materials | Cross-linked polyethylene, EPDM, silicone |
| Termination | Field-shaped silicone overmold with integrated handling boot |
Specifications represent typical values for representative product families. Actual qualification specifications are application-specific and confirmed during program engineering.
- Serialized part marking traceable to build records
- Electrical test report (hi-pot, partial discharge, leakage current) for each unit
- Material certifications and process traceability per AS9100
Where Caton interconnect is specified today
Engineering relationships across HV test equipment and HV power supply manufacturers
Components specified into HV test equipment and HV power supply programs serving industrial, utility, and capital equipment OEM customers. Specific program references available under appropriate disclosure.
Engineering accountability for the parts that hold the voltage
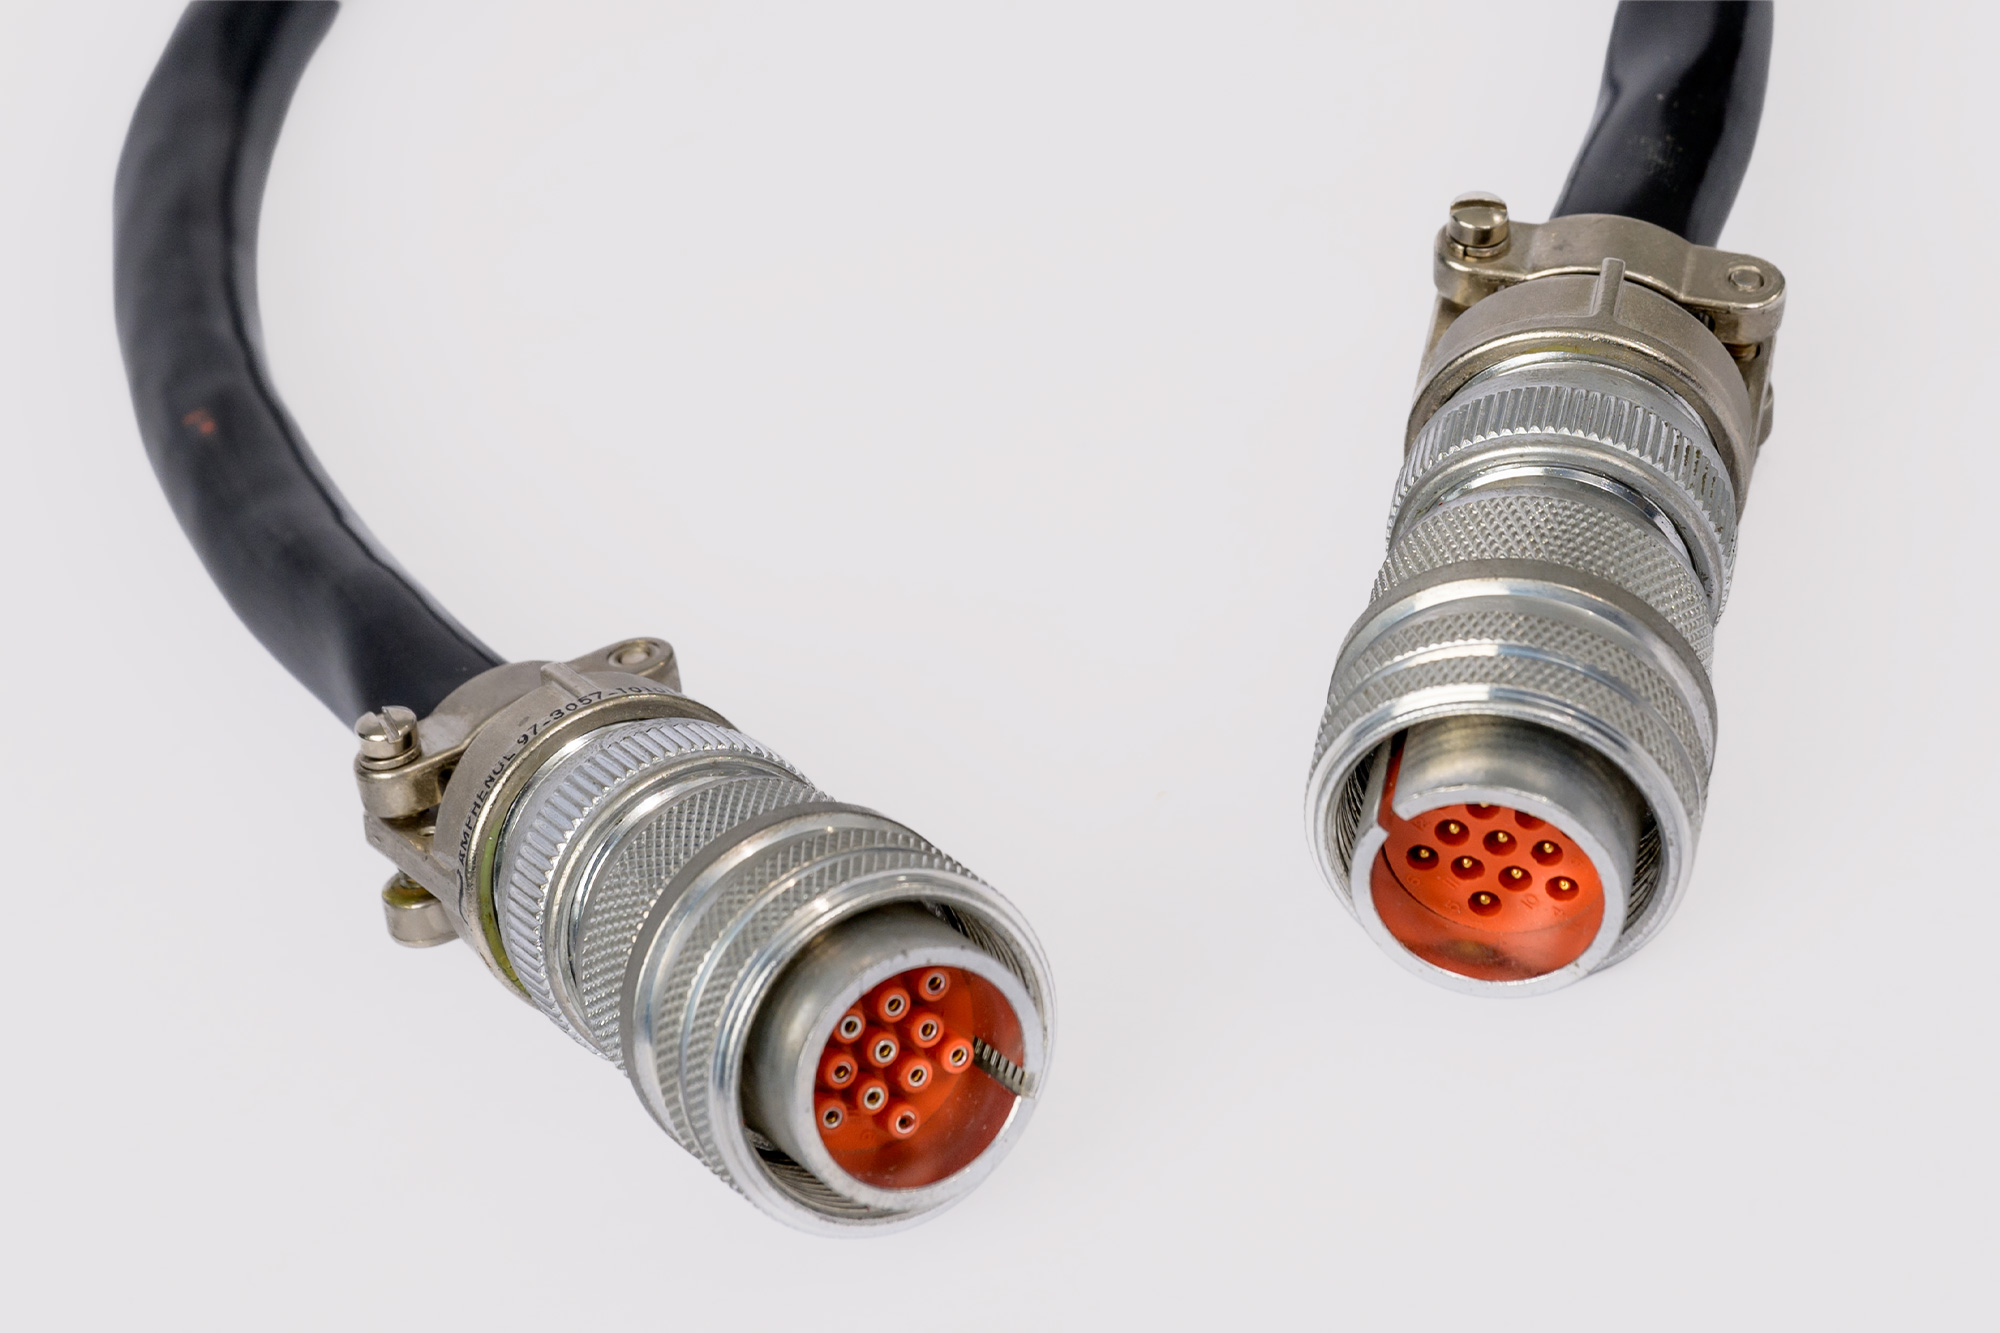
The same engineering group designs the cable, the connector, and the overmold. The dielectric path is one continuous design, not three suppliers' parts mated together — and the test data ships with the part.
At 5–50 kV in air, corona inception is the dominant failure mode and most catalog cable won't hold the operating voltage on a long lead. Caton designs the geometry to hold, qualifies it on the bench to 100 kV hi-pot, and ships data with the part. You don't find out at the substation.
Test equipment and HV power supply programs run on tight build schedules and the cable supplier is often the long pole. Caton's full in-house design, build, and test capability means we don't wait on a sub-tier connector house. Standard programs ship in weeks, not months.
Your design engineer talks to our design engineer. No account manager translation layer, no “I'll have to check with engineering.” The answer comes from the person who can change the design.
Test leads get dragged across plant floors, wound on reels, and connected by gloved hands at substations. Overmold geometry, durometer, and strain relief are engineered for that environment — not adapted from a benchtop part. Cycle and handling life are qualified, not assumed.
Working with Caton on an industrial power or test program
We're built for the design phase of new test sets and HV power supply platforms, and for the recovery phase of existing programs where the incumbent cable supplier can't hold corona, can't hit lead time, or can't deliver overmolded terminations that survive the field. The earlier we're engaged, the more design margin we can build in. We respond to RFQs at the prototype, qualification, and production stages, and we support sustainment and obsolescence on legacy equipment.
Explore other industries we serve
Talk to engineering about your industrial program
Your design engineer talks to our design engineer. New test set or HV power supply development, qualification recovery, sustainment, or obsolescence on legacy equipment — the conversation starts at the engineering bench.